Triple-Offset Butterfly Valves (TOV)
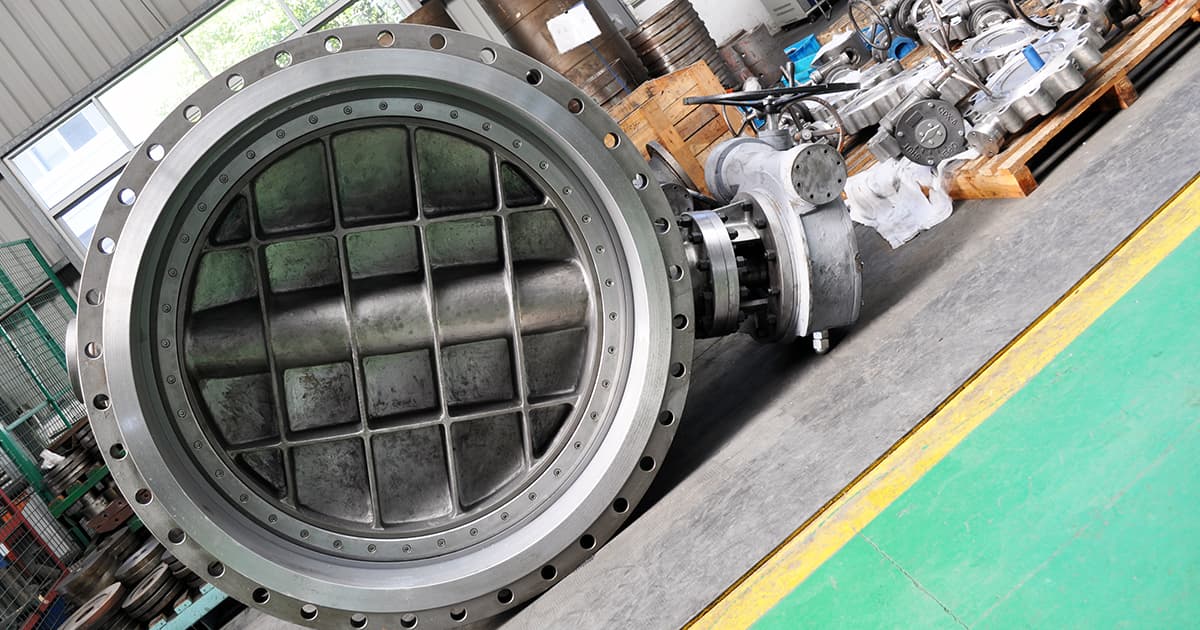
Zero-leakage triple-offset design available double flanged (short and long pattern), butt weld, lug, or wafer type, from 1/2" to 60" and Class 150 to 600.
Size Range
1/2" – 60"
Class Range
150 – 600
Reference
Design Standard
- API 609 Category B
Face to Face
- API 609
- MSS SP-68
- ISO 5752
- BS EN 558
Flange
- ASME B16.5
- ASME B16.47
- BS EN 1092
Top Flange
- ISO 5211
Pressure & Temp.
- ASME B16.34
Fire Safe Design
- API 6FA
- API 607
Pressure Testing
- API 598
Fugitive Emission
- MESC SPE 77/300
- EPA 21
Design Features
- —Triple-offset elliptical sealing geometry delivers bi-directional, zero-leakage shutoff with minimal seat wear, even after extensive cycling
- —Torque-induced sealing: the tighter the closing torque, the tighter the seal
- —Anti-blowout stem with three independent retention methods
- —Graphite performance packing meets low fugitive-emissions requirements
- —Choice of laminated seal ring (mild-severe service) or solid seal ring (severe service with entrained debris)
- —Available in wafer, lug, and double-flange body styles
- —Precision-machined bearings minimize drive-train friction, transferring more of the input torque to the sealing faces
- —ISO 5211 top flange for ease of actuation
Materials Available
Casting Material
- WCB
- LCB
- WC6
- WC9
- C5
- C12
- CF3
- CF3M
- CF8
- CF8M
- C95500
- 4A
- 5A
- Inconel 825/625
Forging Material
- A105
- LF2
- F11
- F12
- F304
- F321
- F347
- F316
- 304L
- 316L
- C61900
- F51
- F53
- F55
- Inconel
Literature
Select what you'd like below and we'll email you secure download links.
Catalogue
Snapshot & One-Pager
Unique to Ranger
High-Pressure Pneumatic Shell Test
For all cast steel gate, globe, and check valves, as well as cast trunnion and floating ball valves, RANGER-FZV submerges the completed, uncoated valve in water and pressure tests the casting with nitrogen or compressed air. Pinholes or casting deficits invisible to a standard hydrotest are revealed as bubbles in the water — castings have failed this test after passing hydrotest.
View full Casting Quality program →