Quality Control
Repeatable quality, by process
RANGER-FZV is dedicated to the design and manufacture of high-quality valves for a range of heavy industrial applications, with a rigorous program for continuous improvement.
Quality Management System
RANGER-FZV's Quality, Environment, Health and Safety (QEHS) management system incorporates ISO 9001:2015, API Spec Q1, ISO 14001:2015, and ISO 45001:2018, covering the full product realization cycle — contract and requirements review, design and development with documented verification and validation, control of externally provided processes and products, production and servicing, and control of nonconforming outputs. Performance is evaluated through internal audits and management review conducted at least annually, with documented corrective and preventive action processes.
Governing Design Standards
| Standard | Scope |
|---|---|
| ASME B16.34 | Flanged, threaded, and welding-end valve design |
| ASME B16.5 / B16.47 | Pipe flanges and flanged fittings |
| ASME B16.10 | Face-to-face and end-to-end dimensions |
| ASME B16.25 | Buttwelding ends |
| ASME BPVC II, V, VIII, IX | Materials, NDE, pressure design, and welding qualification |
Supply Chain & Material Traceability
Approved Material Sources
Castings and forgings are sourced from an approved, audited supplier base, classified and scored on quality, delivery, price, and cooperation, with audit frequency adjusted by performance.
Melting & Material Quality
Castings are produced from master heats, electric-furnace melted with AOD/VOD/VIM ladle refining and forced aluminum deoxidation, with scrap screened for radioactive contamination before melting. Forgings are produced from electric-furnace ingot or continuous-cast billet with enforced minimum reduction ratios. Castings receive periodic radiography, with repairs documented per qualified weld procedures.
Traceability
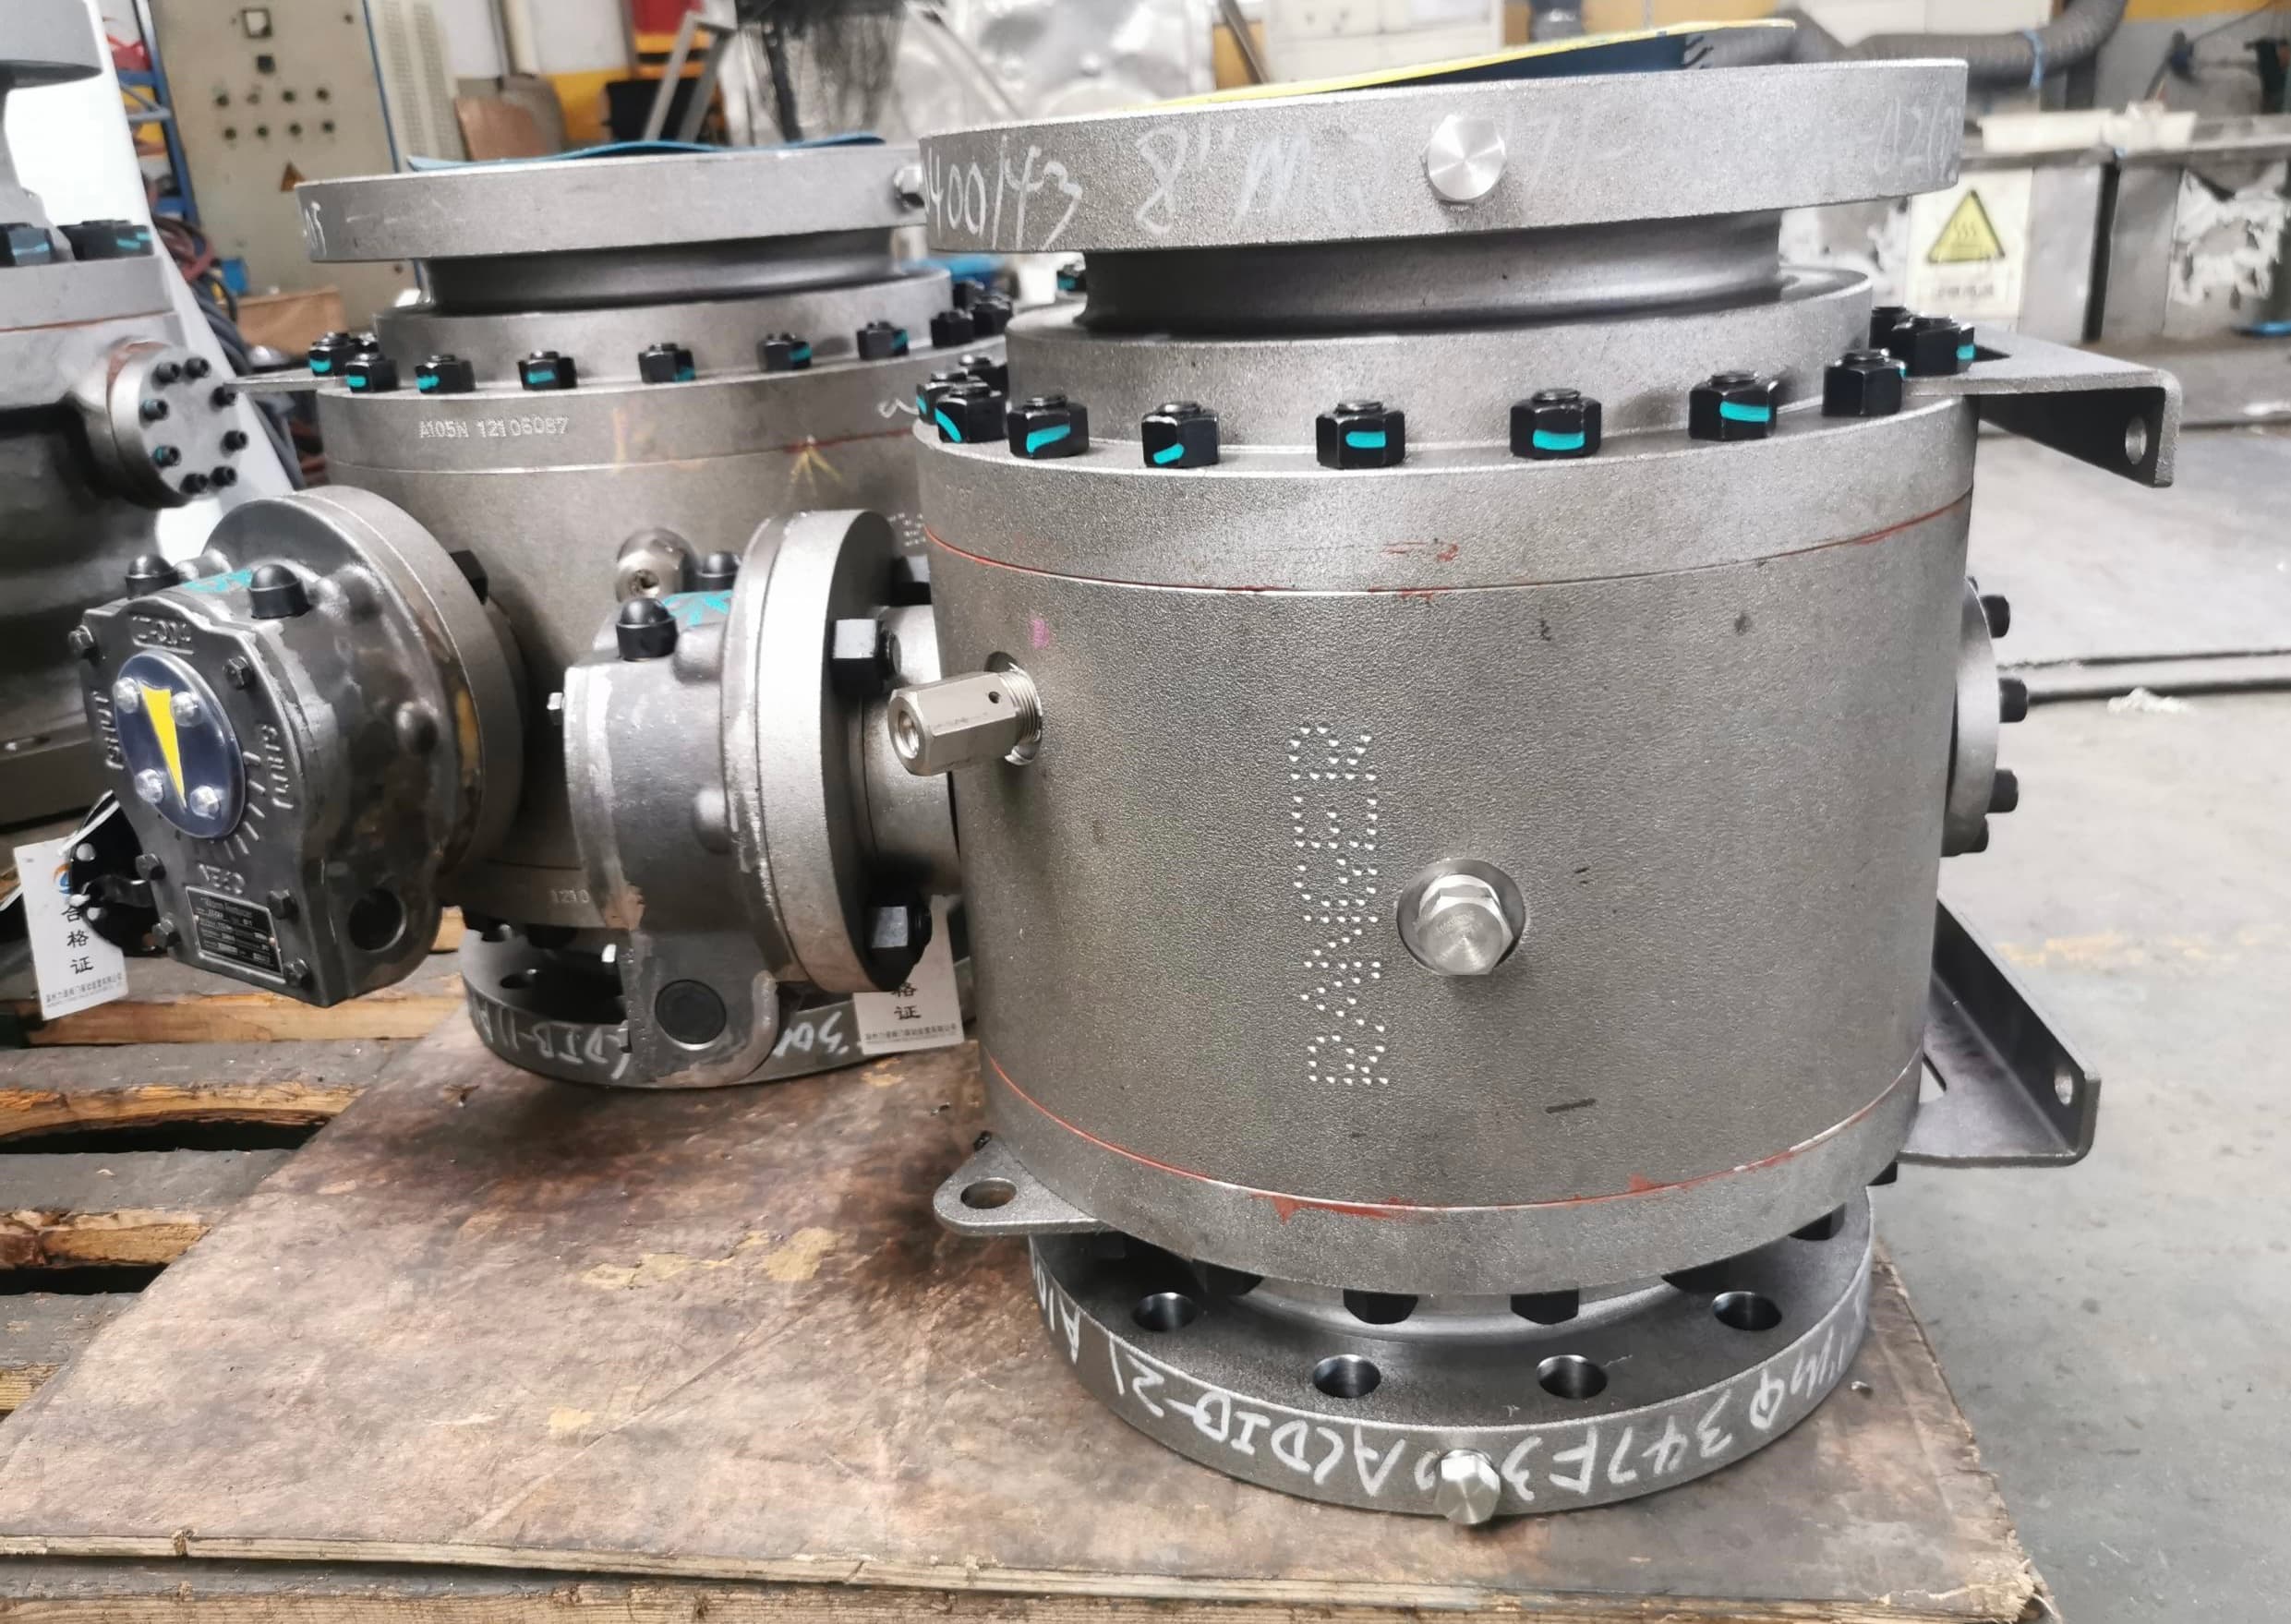
Heat number, material grade, size, and order number are cast, forged, marked, or punched on every part and verified against mill test certificates at receipt. Traceability cards accompany parts through production, with raw material stored segregated by grade and order. Chemistry is verified by OES and 100% PMI at every stage of manufacture, with certified material test reports delivered electronically per EN 10204 3.1 (3.2 with third-party witness on request).
Storage & Export Packing
2,000 m² of covered storage and 5,000 m² of open storage, with export packing in heat-treated, seaworthy wooden crates performed on premises.
Manufacturing & Special Processes
Clean Room Assembly
A dust-free, controlled environment dedicated to oxygen and cryogenic service valve assembly, where foreign material can compromise sealing performance.
Welding
SMAW, SAW, GMAW, GTAW, plasma, weld overlay, and hard facing are all performed in-house — no welding is subcontracted. Welders and procedures are qualified to ASME Section IX, with filler metals selected per ASME Section II and a WPS/PQR system covering a broad range of base materials from 1.5mm to 60mm thickness (unlimited for overlay), with PQR accuracy certified by third-party inspection.
Heat Treatment
Normalizing, tempering, quenching, annealing, PWHT, and local stress relief are performed in-house in thermocouple-controlled electric furnaces with recorded charts, and validated by microstructure analysis. Hot forging is never credited as heat treatment.
Coating & Preservation
The standard system is grit blast, ultrasonic clean and dry, then primer, intermediate, and finish coats, with galvanizing, phosphating, and PTFE coating available. Valve ends and internals are protected with covers designed to prevent installation before removal.
Inspection & Testing
RANGER-FZV operates its own in-house laboratory for research, development, and testing, and offers additional or special testing as required by customers. Every stage of production, from incoming material to final shipment, is independently verified:
Material Review
Tensile, Charpy impact, and hardness testing per ASTM A370 on coupons removed from production castings and forgings — one test per heat per heat-treatment load, with coupon linkage verified by heat number. A failure triggers two additional random specimens; persistent failure results in quarantine and return of material to the supplier. Hardness is checked 100% on coupons escalating to parent material, with in-house metallography and third-party intergranular corrosion testing.
Non-Destructive Examination (NDE)
UT, MT, PT, and PMI performed in-house by ASNT SNT-TC-1A qualified personnel, to ASME V, ASME VIII, and B16.34, with casting surfaces inspected to MSS SP-55. Radiography is performed by qualified subcontract NDE laboratories.
Special Testing
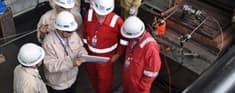
Cryogenic, high-temperature, and high-pressure gas closure testing available on request, with third-party witness testing accommodated.
Pressure Testing & Final Inspection
Every valve is shell and closure tested after final machining and assembly — never delegated to the foundry — with backseat testing performed where applicable and high-pressure liquid closure and gas testing available on request. Final inspection includes 100% torque check, 100% visual inspection, and dimensional sampling at 10% per order item per lot, plus coating, packing, and fugitive-emission testing when specified, with documentation per EN 10204 3.1 (3.2 with third-party witness on request).
Third-Party Inspection
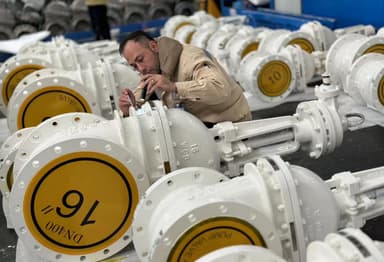
RANGER-FZV routinely hosts customer and third-party inspection for witness of pressure tests, NDE, and documentation review, and accommodates additional witness requirements as directed by the customer.
RANGER-FZV Casting Quality
Visual, shell, mechanical & documentation review
For cast steel gate, globe, and check valves, as well as cast trunnion and floating ball valves, every casting is reviewed against this checklist before it leaves the foundry.
100% Raw Material Certificates Check
Material certificates are checked for tensile and hardness properties, chemical composition, heat treatment (temperature, holding time, cooling method), and an authorized signature.
10% Dimensional Inspection
Wall thickness and external dimensions are verified correct.
Magnetic Particle Testing
Standard on one piece from every heat batch.
PMI of Every SS and Alloy Heat
Positive material identification is conducted on all stainless steel and alloy materials.
100% Shell Hydrotest at 150% of Rated Pressure
A shell hydrotest is conducted per API specification, including pressure and duration.
100% Appearance & Marking Check
A visual review of casting appearance per MSS SP-55 for cracks, gas porosity, sand inclusions, excess metal, or major repairs, plus a clarity check of all markings.
Unique to Ranger
High-Pressure Pneumatic Shell Test
For all cast steel gate, globe, and check valves, as well as cast trunnion and floating ball valves, RANGER-FZV submerges the completed, uncoated valve in water and pressure tests the casting with nitrogen or compressed air. Pinholes or casting deficits invisible to a standard hydrotest are revealed as bubbles in the water — castings have failed this test after passing hydrotest.
Test Duration by Size
| NPS | Duration (min.) |
|---|---|
| 1/2" – 4" | 4 |
| 6" – 10" | 10 |
| 12" – 18" | 20 |
| ≥ 20" | 30 |
Test Pressure by Class
| Class | Pressure (psi) |
|---|---|
| 150 | 300 |
| 300 | 575 |
| 600 | 725 |
| 900 | 725 |
| 1500 | 2175 |
| 2500 | 3625 |
Specifications
Trim, seat, and seal materials, and standards, size and pressure ranges, and casting and forging materials by product segment.
Trim Material
- A105 + ENP
- LF2 + ENP
- F304
- F316
- F51
- F55
Seat & Seal Material
Resilient
- TFE
- RPFE
- PEEK
- Nylon
- PCTFE
- Molon
- Devlon
- Delrin
Metal
- Stellite
- 13 Cr
- Inconel
- Monel
Trim / Seal Facing / Stem Reference
| Trim | Seal Facing | Stem |
|---|---|---|
| #1 | 13 Cr | 13 Cr |
| #8 | 13 Cr / STL | 13 Cr |
| #5 | STL | 13 Cr |
| #2 | 304 | 304 |
| #10 | 316 | 316 |
| #12 | 316 / STL | 316 |
| #9 | Monel | Monel |
Mid & Downstream Products
Key standards and product information for oil and natural gas pipelines.
Standard
- API
- ANSI
- ASME
- ASTM
- MSS
- ISO
- BS
Size & Pressure Range
- Class 150 – 6001/2" – 60"
- Class 900 – 15001/2" – 32"
- Class 25001/2" – 24"
Casting Material
- WCB
- LCB
- WC6
- WC9
- C5
- C12
- CF3
- CF3M
- CF8
- CF8M
- C95500
- 4A
- 5A
- Inconel 825/625
Forging Material
- A105
- LF2
- F11
- F12
- F304
- F321
- F347
- F316
- 304L
- 316L
- C61900
- F51
- F53
- F55
- Inconel
Upstream Products
Overview of products manufactured for wellhead applications.
Standard
- API 6A
- API 16C
- and other relevant specifications
Size & Pressure Range
- 2,000 – 15,000 psi1-1/16" (46mm) – 13-5/8" (350mm)
Casting Material
- A487 4C
- A487 Gr9
- CA-15
- and other equivalents
Forging Material
- AISI 4130
- AISI 4135
- AISI 4140
- AISI 1040
- AISI 1045
- 410SS
- 17-4PH
- Inconel 718
- Inconel 625
Design Features
- —Fire-safe certified designs, with anti-static devices available
- —Blowout-proof stems — not removable under pressure by removal of the gland alone
- —Automatic cavity pressure relief on applicable trunnion designs
- —Position stops and tamper-proof position indicators on quarter-turn valves
- —Wafer and flanged valves rated for dead-end service at full differential pressure
- —Flow coefficient (Kv), breakaway torque, and maximum allowable stem torque supplied by design calculation and verified by measurement
- —Locking devices, gear operators, extended levers, and bare-shaft actuator-ready configurations available